Business Details
50+ Years
experience
Your Trusted Partner for Industrial Control Valve Solutions
Nbal Valves has been at the forefront of developing advanced automatic control valves and systems since 1971. Our pioneering spirit was demonstrated in 1974 with the introduction of the world's first N.M.M.P. (No Moving Mechanical Parts) automatic control valve, revolutionising the industry. With over five decades of experience, we specialise in designing and manufacturing control valves for fire protection applications across offshore platforms, oil refining, petrochemical, marine, aviation, and power generation sectors. Our commitment to innovation is matched by our dedication to reliability, as evidenced by our ISO 9001 certification since 1991 and additional certifications for occupational health and safety (ISO 45001) and environmental management (ISO 14001).We provide tailored solutions that meet specific customer requirements, including custom applications, technical documentation, and global after-sales support. Our valves are rigorously tested to ensure performance under real-world conditions, and we maintain full compliance with international standards through our comprehensive quality assurance processes. With installations in over 50 countries, our reputation as a global leader in control valve technology is built on a foundation of technical excellence and customer-centric service.
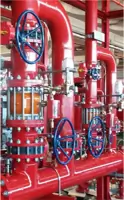
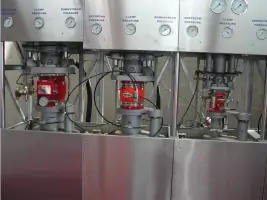
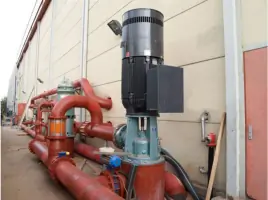
Services
Deluge Valves
Pressure Control Valves
Dry Pipe Valves
Preaction Valves
Remote Control Valves
Pressure Reducing Valves
Pressure Relief Valves
Differential Control Valves
Foam Concentrate Valves
Customized Products
Details
- Year established: 1971
Highlights and features
- We have over 50 years of experience in industrial valve technology since 1971
- Our patented N.M.M.P. design eliminates mechanical failure risks in critical systems
- We maintain ISO 9001, ISO 45001, and ISO 14001 certifications for quality and safety
- Our global presence spans installations in over 50 countries worldwide
- We provide custom-engineered solutions with comprehensive technical support
Associations and certifications
- ISO 9001
- ISO 45001
- ISO 14001
- Underwriters Laboratories (UL)
- Factory Mutual (FM)
- Lloyds Register (LR)
- American Bureau of Shipping (ABS)
- Bureau Veritas (BV)
- Det Norske Veritas Germanischer Lloyd (DNV GL)
Services
Deluge Valves
Our deluge valves provide rapid water distribution in fire protection systems. Designed with N.M.M.P. technology, they eliminate mechanical failure risks while ensuring immediate response to fire events. These valves maintain drip-tight seals under pressure and open smoothly to prevent water hammer, making them ideal for high-risk environments like offshore platforms and chemical storage facilities.
Pressure Control Valves
Precision-engineered pressure control valves maintain consistent water pressure in fire protection systems. Our patented sleeve actuator design automatically adjusts to inlet pressure fluctuations while maintaining pre-set delivery pressure. This ensures reliable operation in critical applications across petrochemical plants and power generation facilities where pressure stability is essential.
Dry Pipe Valves
Dry pipe valves protect against water damage in non-pressurized fire suppression systems. Our solution features corrosion-resistant materials and a unique sealing mechanism that prevents false tripping in extreme temperatures. These valves are specifically designed for cold environment applications in warehouses and transportation tunnels where freezing conditions exist.
Preaction Valves
Preaction valve systems combine fire detection and suppression in a single solution. Our design integrates with electrical detection systems while maintaining mechanical reliability through N.M.M.P. technology. This dual protection approach prevents water discharge until actual fire conditions are confirmed, reducing water damage risks in sensitive environments.
Foam Concentrate Valves
Specialised foam concentrate valves control fire suppression chemical distribution. Constructed from corrosion-resistant materials like stainless steel and titanium, these valves handle aggressive foam agents while maintaining precise flow control. They are engineered for marine and aviation applications where flammable liquid fires require rapid chemical suppression.
Questions
What makes Inbal Valves different from conventional control valves?
Our patented N.M.M.P. (No Moving Mechanical Parts) design eliminates mechanical failure points found in traditional valves, ensuring reliable operation in critical fire protection systems without maintenance issues.
Which industries benefit most from your valve technology?
We specialise in serving offshore platforms, marine facilities, aviation infrastructure, oil & gas operations, petrochemical plants, and power generation facilities requiring reliable fire protection systems.
What certifications do your products hold?
Our valves are certified by Underwriters Laboratories (UL), Factory Mutual (FM), and multiple maritime classification societies. We maintain ISO 9001, ISO 45001, and ISO 14001 certifications for quality and safety.
Can you provide customised valve solutions?
Yes, our engineering team designs custom valve systems to meet specific project requirements, including material selection, pressure ratings, and integration with existing fire protection infrastructure.
How do you ensure product reliability under extreme conditions?
All valves undergo full-flow testing under simulated operating conditions. Our design withstands pressure surges and operates effectively in temperatures ranging from Arctic cold to desert heat.