Business Details
Trusted Industrial Flooring & Refractory Solutions
Ancorite Surface Protection is a leading provider of industrial flooring, refractory linings, and anti-corrosive solutions with decades of experience in demanding environments. As part of the Steuler Group, we combine global expertise with local execution to deliver tailored, high-performance systems for sectors including pharmaceuticals, petrochemicals, and food and beverage. Our holistic approach integrates resin coatings, terrazzo flooring, ceramic tiling, and GRP pipework, supported by a commitment to innovation, technical excellence, and client collaboration.With operations across the UK, Ireland, and internationally, we prioritise rapid mobilisation, minimising downtime while maintaining rigorous quality and safety standards. Our team of specialists ensures every project, from small repairs to large-scale installations, meets exacting specifications and exceeds industry expectations.
Services
Flooring
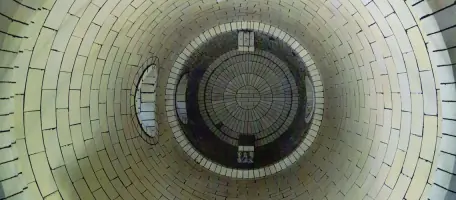
Refractory Linings
Vessels
Pipework
Ancillary Items
Terrazzo Flooring
Ceramic Tiling
GRP Systems
Rubber Linings
Anti-Corrosive Linings
Highlights and features
- Decades of experience in demanding industrial environments
- Global reach supporting clients in 6 continents
- Rapid mobilisation to minimise downtime and disruptions
- Tailored solutions combining resin coatings, linings, and pipework
- Part of the Steuler Group with access to advanced technologies
What people say
Exceptional quality
Professionalism and expertise
Seamless process
Outstanding workmanship
Meets safety standards
Services
Refractory Linings
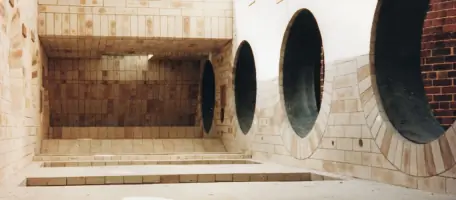
Ancorite delivers high-temperature refractory solutions for industrial furnaces and chemical processing equipment. Our services include brickwork installation, castable linings, and ceramic fibre systems designed to withstand extreme thermal stress. With expertise in petrochemical, steel, and incineration sectors, we provide materials selection, installation, and maintenance that extends asset life while maintaining operational safety and efficiency.
Terrazzo Flooring
Our polyurethane and epoxy terrazzo systems combine durability with aesthetic appeal for commercial and industrial spaces. Featuring anti-static properties and seamless finishes, these floors resist chemical exposure and heavy foot traffic. Customisable designs using glass, marble, or quartz aggregates make them ideal for retail environments, healthcare facilities, and pharmaceutical plants requiring both functionality and visual impact.
GRP Pipework
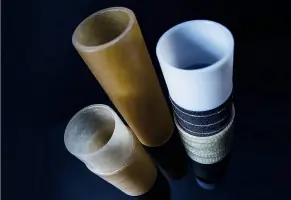
Ancorite's glass-reinforced plastic (GRP) and GRE pipework systems offer corrosion-resistant solutions for aggressive chemical environments. We provide spiral-wound GRP pipes, pressure-rated GRE lines, and custom fabrication of bends and fittings. These systems meet ISO standards for water treatment plants, chemical distribution networks, and utility pipelines, ensuring long-term performance with minimal maintenance requirements.
Ceramic Tiling
We specialise in vibration, traditional, and chemical-resistant tiling methods for food processing, pharmaceutical, and automotive sectors. Our systems use vitrified tiles with epoxy grouts to create impervious surfaces that withstand mechanical stress and frequent cleaning. The Vibro HD system incorporates anti-static membranes for critical cleanroom environments, while CR tiling provides chemical protection in solvent-exposed areas.
Resin Coatings
Ancorite's epoxy and polyurethane resin coatings protect industrial floors from abrasion, chemical attack, and thermal shock. Available as anti-slip quartz aggregates or decorative flake finishes, these systems range from 2mm to 9mm thickness for heavy-duty applications. We provide stainless steel drainage integration and coving installations to meet hygiene standards in nuclear, food processing, and pharmaceutical facilities.
People
Tom Dossett
Technical Sales Manager
With 15+ years in industrial coatings, Tom leads technical sales, providing expert specification advice for complex flooring and lining projects across the UK.
Ryan Hall
Contracts Manager
Ryan manages large-scale refractory projects from the Teesside office, bringing 12 years of experience in coordinating multidisciplinary teams for petrochemical clients.
Jon Lax
Contracts Manager
Based in Beverley, Jon oversees commercial flooring contracts, specialising in delivering hygienic resin systems for food and beverage sector clients.
Tony Cosgrove
Contracts Manager
Tony manages operations from the Mayo office, focusing on Irish market projects with expertise in GRP pipework and anti-corrosive linings.
Questions
What industries does Ancorite serve?
Ancorite supports pharmaceutical, petrochemical, food and beverage, power generation, and other industrial sectors with tailored flooring and lining solutions.
Are Ancorite's solutions suitable for hygienic environments?
Yes, our resin coatings and terrazzo flooring systems meet stringent hygiene requirements for pharmaceutical and food processing facilities.
Can Ancorite handle international projects?
With global reach across six continents, we deliver turnkey solutions supported by local teams and Steuler Group resources.
What makes Ancorite's flooring systems durable?
We use chemical-resistant materials, anti-slip finishes, and advanced installation techniques to ensure longevity in harsh environments.
Do you offer maintenance services?
Yes, we provide planned and reactive maintenance for flooring, linings, and pipework systems to minimise operational disruptions.
How quickly can Ancorite mobilise for urgent projects?
Our rapid response teams typically mobilise within 24-48 hours to address critical repair or installation needs.
Reviews (1)
Mesfin Gashawbeza
Aug 12, 2014
Report
I am working currently as a freelancer at MACCFA Freight Logistics PLC, Ethiopia. The company is out sourced by Diageo/Meta Ethiopia. Diageo/Meta buys some products of yours and we are going to clear it out from port of Djibout to the factory site at Sebata. I like to google and searched for Anchorite and seeing you. Glad working with you. Mesfin